Sizing a Commercial Post-Harvest Line (kg/hr): Matching Stem Bucker, Tumbler Trimmer, Heat-Pump Dryer & Sorter
How to calculate wet-to-dry mass balance (4.5:1) so your bucking (BE-HV-02), trimming (BE-HV-01), drying (BE-HV-03), and sorting (BE-HV-04) machines never bottleneck harvest week.
The Practical Reality & Process Physics
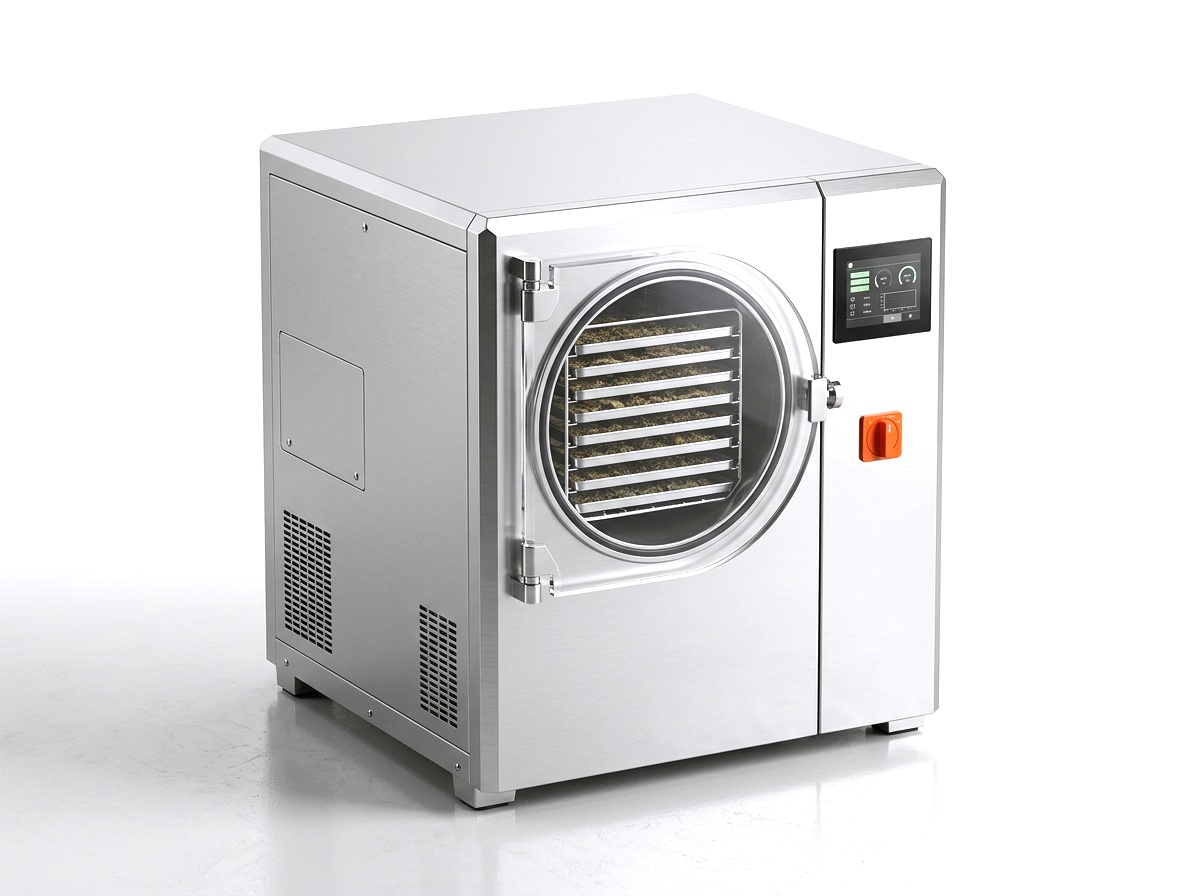
Harvest week bottlenecks occur when facilities buy post-harvest machines with mismatched hourly capacities, forgetting the 4.5:1 wet-to-dry moisture reduction ratio. Freshly harvested cannabis or hemp flower contains 78% to 82% water: 300 kg of wet bucked flower entering your drying room exits as roughly 65 kg of dry cured flower at 11% moisture.
If your facility harvests 250 to 350 kg of wet flower per day: one BE-HV-02 Stem Bucker (25-65 kg/hr wet) strips the day's harvest off the stalks in 6 hours. If you wet-trim before drying, one BE-HV-01 Commercial Tumbler Trimmer (15-45 kg/hr wet) keeps pace in real time while its cyclone separator captures wet sugar trim into a dedicated collection bag. The entire 300 kg wet batch then loads onto the 48-to-96 stainless mesh trays of a single BE-HV-03 Low-Temperature Heat-Pump Dryer.
Once dried to 11% water activity (0.58-0.62 aw) over 48 to 72 hours at 20 C - 32 C inside BE-HV-03, the 65 kg dry batch is finished in 6 hours on the dry drum of BE-HV-01 (4-12 kg/hr dry) and graded in 60 minutes on the BE-HV-04 4-Tier Size Sorter (40-120 kg/hr)—sending A-grade tops and B-grade mids to the BE-PK-04 Jar Line and sending smalls/shake directly to the BE-HV-05 Cold-Mill Grinder for pre-rolls.
Reference Operating Window & Numbers
| Parameter | Specification |
|---|---|
| Wet-to-Dry Shrinkage Ratio | 4.5 : 1 (300 kg Wet -> ~66 kg Dry Flower) |
| Drying Cycle (BE-HV-03) | 36 - 72 Hours Closed-Loop @ 20-35 C |
| Trimmer Match (BE-HV-01) | 1 Tumbler per 1.5 Stem Buckers |
| Sorter Output (BE-HV-04) | 40 - 120 kg/hr Dry Graded Flower |
Step-by-Step: How to Do It Right on the Floor
Step 1: Define Your Material & Target Spec (Wet-to-Dry Shrinkage Ratio: 4.5 : 1 (300 kg Wet -> ~66 kg Dry Flower))
Before touching a machine switch, measure your starting material and target container or batch geometry. In this workflow, holding Wet-to-Dry Shrinkage Ratio within 4.5 : 1 (300 kg Wet -> ~66 kg Dry Flower) is the difference between a repeatable commercial run and a batch you have to rework by hand. Log your viscosity, moisture content, or dimensional tolerance on a single batch sheet before warming up the line.
Step 2: Lock Your Thermal & Mechanical Envelope (Drying Cycle (BE-HV-03): 36 - 72 Hours Closed-Loop @ 20-35 C)
Set your PID temperature controllers, pressure regulators, or screen clearances to stabilize at 36 - 72 Hours Closed-Loop @ 20-35 C for at least 15 minutes before feeding product. Cold stainless steel steals heat from the first 50 units; letting the manifold or jacketed wall reach thermal equilibrium ensures unit #1 and unit #1,000 behave identically.
Step 3: Run a Dry & Wet Calibration Pass (Trimmer Match (BE-HV-01): 1 Tumbler per 1.5 Stem Buckers)
Never launch a full shift blindly. Run a 10-unit or 5-liter calibration check at your target cadence (1 Tumbler per 1.5 Stem Buckers), weigh the output on a 0.01 g analytical balance, and inspect seals, trichome integrity, or droplet dispersion under bright white light.
Step 4: Close the Loop Within the Critical Window (Sorter Output (BE-HV-04): 40 - 120 kg/hr Dry Graded Flower)
Complete downstream sealing, curing, filtration, or nitrogen packaging while your product is still inside the optimal physical window (40 - 120 kg/hr Dry Graded Flower). Clean contact parts immediately at shift end while residues are still warm so tomorrow's batch starts with zero cross-contamination.
Comparing All Your Options: What Exists & What Fits Your Scale
| Option / Approach | Realistic Daily Output | Where It Shines (Pros) | Where It Hurts (Limits & Trade-offs) | Who Should Choose This |
|---|---|---|---|---|
| Manual Heated Glass Syringe / Hand-Trigger Gun | 300 - 800 units / day | Lowest cost; quick flavor switches for 50-unit sample runs. | Severe wrist fatigue; shot weight drifts +/- 5% as the barrel cools; slow manual capping causes chimney flooding. | R&D sampling or micro-batches under 1,000 units per week. |
| Single-Nozzle Benchtop Heated Filler (BE-VF-15 / BE-VF-27) + Manual Arbor Press | 2,000 - 4,500 units / day | Digital servo dosing (+/- 0.5%) with heated reservoir and needle; fast 10-minute terpene changeover. | Operator still indexes one tray row by hand; capping is a separate manual lever stroke. | Single-operator labs producing 5,000 to 15,000 cartridges per week across multiple strains. |
| 5-Channel Heated CNC Gantry (BE-VF-28) + 100-Cavity CNC Aluminum Trays + 100-Unit Platen/Torque Capper (BE-VC-29 / BE-VC-30) | 15,000 - 28,000 units / day (3,600/hr) | Fills 100 cartridges in 70 seconds (5 needles at once); shared CNC aluminum tray transfers directly into the 100-cavity capper within the 90-second anti-leak window. | Requires custom CNC aluminum trays milled to your device CAD (+/- 0.02 mm). | Commercial processors running 15,000 to 100,000+ units per week who want zero leaks and 1-operator efficiency. |
| Fully Automated Rotary Monoblock (Auto-Feeder + Fill + Cap + Label) | 35,000+ units / day | Unattended continuous feed for a single locked hardware SKU. | Takes 4-6 hours to re-tool if you change pod shapes; 4x higher capital cost. | High-volume co-packers running millions of identical 510 carts with zero hardware changes. |
How to Decide: The 4 Critical Decision Points Before You Buy
1. Calculate Your Real Weekly Volume vs. Labor Cost
Do not buy automation for ego, and do not stay manual out of habit. If two operators spend more than 12 hours a week repeating this step by hand, or if scrap/giveaway exceeds 3%, semi-automatic or turnkey equipment pays for itself in 6 to 14 weeks.
2. Match the Machine to Your Hardest Material (4.5 : 1 (300 kg Wet -> ~66 kg Dry Flower))
Anyone can run thin, warm liquids or bone-dry trim. Size and choose your equipment for your most demanding product — whether that is un-cut live rosin, sticky resinous flower, or -40 C solvent washes requiring 36 - 72 Hours Closed-Loop @ 20-35 C.
3. Check Format Changeover Time Before You Buy
If your facility runs five different SKUs or strains a day, a rigid rotary line that takes 4 hours to re-tool will sit idle. Choose modular equipment where trays, screens, or fluid paths swap in under 15 minutes.
4. Demand Proof Before Shipment (Unedited 4K FAT)
Never wire final balance payments on brochure promises. Insist on seeing your exact hardware (BE-HV-02, BE-HV-01, BE-HV-03, BE-HV-04) running your device CAD and facility voltage in an unedited 4K test video before the crate leaves the factory.
Expensive Mistakes Operators Make (and How to Avoid Them)
Ignoring Thermal & Pressure Drift (Wet-to-Dry Shrinkage Ratio)
Allowing Wet-to-Dry Shrinkage Ratio to drift outside 4.5 : 1 (300 kg Wet -> ~66 kg Dry Flower) mid-shift causes immediate viscosity spikes, terpene evaporation, or seal failure. Always use closed-loop PID control rather than manual dial rheostats.
Buying Oversized or Undersized Upstream Prep
A fast machine starved by slow upstream prep — or bottlenecked by slow manual capping/drying downstream — never hits 1 Tumbler per 1.5 Stem Buckers. Balance every step of the cell to the same hourly rhythm.
Skipping Rigid Tooling or Sanitary Connections
Using soft shipping foam, uncalibrated silicone hoses, or non-sanitary threads introduces 36 - 72 Hours Closed-Loop @ 20-35 C alignment errors and microbial traps. Stick to 304/316L stainless steel and CNC-milled 6061-T6 aluminum fixtures.
Questions Buyers & Operators Ask Most
How much electrical power does the BE-HV-03 Closed-Loop Heat-Pump Dryer save compared to traditional vented drying rooms?
Because BE-HV-03 condenses moisture in a closed loop and recycles latent heat back into the chamber rather than exhausting conditioned air outdoors, it cuts kWh consumption by 60% to 70% while preventing terpene loss and outside mold spores.
When should we stay manual vs. upgrading to BE-HV-02, BE-HV-01, BE-HV-03, BE-HV-04?
If you are running small R&D tests once a month, manual tools are fine. The moment you need repeatable 1 Tumbler per 1.5 Stem Buckers output, consistent 36 - 72 Hours Closed-Loop @ 20-35 C precision, and single-operator labor efficiency without batch-to-batch drift, upgrading to BE-HV-02, BE-HV-01, BE-HV-03, BE-HV-04 eliminates the bottleneck.
Can we buy just one machine now and add the rest of the line later?
Yes. Every module (BE-HV-02, BE-HV-01, BE-HV-03, BE-HV-04) is built to operate standalone on standard facility utilities (40 - 120 kg/hr Dry Graded Flower) while sharing the same 100-cavity tray geometry and sanitary Tri-Clamp standards when you scale.
If You Are Building This Line: Matched Modular Equipment
Only after your process and daily volume are clear should you pick hardware. Here are the modules engineered for this exact workflow.
| SKU | Machine | Throughput | 1-Unit (EUR) | Action |
|---|---|---|---|---|
| BE-HV-02 | High-Torque Wet & Dry Stem Bucking / De-Budding Machine | 25 - 65 kg/hr | EUR 2,400 | Cart |
| BE-HV-01 | Commercial Wet & Dry Tumbler Bud Trimming Machine | 15 - 45 kg/hr (wet) / 4 - 12 kg/hr (dry) | EUR 2,800 | Cart |
| BE-HV-03 | Low-Temperature Heat-Pump Tray & Belt Botanical Dryer | 100 - 350 kg wet batch capacity | EUR 6,800 | Cart |
| BE-HV-04 | Multi-Tier Flower Size Sorter & Grade Classifier | 40 - 120 kg/hr | EUR 3,200 | Cart |
What to Read Next
Wet vs. Dry Tumbler Bud Trimming & Stem Bucking Line: Preserving Flower Structure at Scale
How to sequence counter-rotating neoprene stem bucking (BE-HV-02), VFD tumbler trimming (BE-HV-01), and 4-tier size grading (BE-HV-04) so A-grade flower goes to jars and trim goes to pre-rolls.
Closed-Loop Heat-Pump Botanical Dryer (BE-HV-03) vs. Open Hang-Drying Rooms: Terpene & Water Activity Control
Why open HVAC hang-drying rooms suffer from micro-climate mold pockets and terpene venting, and how closed-loop 20-55 C heat-pump dehumidification standardizes water activity (0.58 aw).
Industrial Hemp & Cannabis Post-Harvest Processing Guide: Flower & Extraction Biomass vs. Stalk Fiber
Understanding the engineering boundary between trichome-preserving botanical flower/extraction post-harvest lines (BE-HV-01 to BE-HV-05) and agricultural stalk fiber decortication.